Carbon and manganese are the two most cost-effective alloying additions to increase strength. While effective at strengthening, these additions reduce ductility and toughness, and make welding more challenging.
The practical usage of these grades typically limits the highest strength to no more than 280 MPa. Adding enough carbon and manganese to achieve higher strength results in a product without sufficient ductility for challenging applications, low toughness, and welding difficulty. These products sometimes are referred to as structural steels, and achieve their strength from the mechanism of solid solution strengthening.
Until the commercialization of High Strength Low Alloy steels, the CMn approach was the only option for users to obtain a high strength sheet metal.
Some of the specifications describing uncoated cold rolled Carbon-Manganese (CMn) or structural steels are included below, with the grades typically listed in order of increasing minimum yield strength and ductility. Different specifications may exist which describe hot or cold rolled, uncoated or coated, or steels of different strengths. Many automakers have proprietary specifications which encompass their requirements. Note that ASTM terminology is based on minimum yield strength, while JIS and JFS standards are based on minimum tensile strength. Also note that JIS G3135 does not explicitly state that these grades must be supplied with a C-Mn chemistry. An HSLA approach is satisfactory as long as the mechanical property criteria are satisfied.
ASTM A1008M, with the terms Grade 25 [170], Grade 30 [205], Grade 33 [230] Type 1, Grade 33 [230] Type 2, Grade 40 [275] Type 1, Grade 40 [275] Type 2, Grade 45 [310], Grade 50 [340], Grade 60 [410], Grade 70 [480], and Grade 80 [550] A-25
JIS G3135 with the terms SPFC340, SPFC370, SPFC390, SPFC440, SPFC490, SPFC540, and SPFC590 J-3
JFS A2001, with the terms JSC340W, JSC370W, JSC390W, and JSC440W J-23
Carbon-Manganese Steels (CMn) are a lower cost approach to reach up to approximately 280MPa yield strength, but are limited in ductility, toughness and welding.
Increasing carbon and manganese, along with alloying with other elements like chromium and silicon, will increase strength, but have the same challenges as CMn steels with higher cost. An example is AISI/SAE 4130, a chromium-molybdenum (chromoly) medium carbon alloy steel. A wide range of properties are available, depending on the heat treatment of formed components. Welding conditions must be carefully controlled.
The 1980s saw the commercialization of high-strength low-alloy (HSLA) steels. In contrast with alloy steels, HSLA steels achieved higher strength with a much lower alloy content. Lower carbon content and lower alloying content leads to increased ductility, toughness, and weldability compared with grades achieving their strength from only solid solution strengthening like CMn steels or from alloying like AISI/SAE 4130. Lower alloying and elimination of post-forming heat treatment makes HSLA steels an economical approach for many applications.
This steelmaking approach allows for the production of sheet steels with yield strength levels now approaching 800 MPa. HSLA steels increase strength primarily by micro-alloying elements contributing to fine carbide precipitation, substitutional and interstitial strengthening, and grain-size refinement. HSLA steels are found in many body-in-white and underbody structural applications where strength is needed for increased in-service loads.
These steels may be referred to as microalloyed steels, since the carbide precipitation and grain-size refinement is achieved with only 0.05% to 0.10% of titanium, vanadium, and niobium, added alone or in combination with each other.
HSLA steels have a microstructure that is mostly precipitation-strengthened ferrite, with the amount of other constituents like pearlite and bainite being a function of the targeted strength level. More information about microstructural components is available here.
Some of the specifications describing uncoated cold rolled high strength low alloy (HSLA) steel are included below, with the grades typically listed in order of increasing minimum yield strength and ductility. Different specifications may exist which describe hot or cold rolled, uncoated or coated, or steels of different strengths. Many automakers have proprietary specifications which encompass their requirements. Note that ASTM, EN and VDA terminology is based on minimum yield strength, while JIS and JFS standards are based on minimum tensile strength. Also note that JIS G3135 does not explicitly state that these grades must be supplied with an HSLA chemistry. A C-Mn approach is satisfactory as long as the mechanical property criteria are satisfied.
ASTM A1008M, with the terms HSLAS 45[310], 50[340], 55[380], 60[410], 65[450], and 70[480] along with HSLAS-F 50 [340], 60 [410], Grade 70 [480] and 80 [550]A-25
EN10268, with the terms HC260LA, HC300LA, HC340LA, HC380LA, HC420LA, HC460LA, and HC500LAD-5
JIS G3135, with the terms SPFC340, SPFC370, SPFC390, SPFC440, SPFC490, SPFC540, and SPFC590J-3
VDA239-100, with the terms CR210LA, CR240LA, CR270LA, CR300LA, CR340LA, CR380LA, CR420LA, and CR460LAV-3
Advanced High Strength Low Alloy (AHSLA) Cold Rolled Steels
Advanced High Strength Steels are a common approach that autobody engineers use for applications requiring grades with yield strength exceeding 500 MPa. Steelmakers increasingly offer alternatives based on High Strength Low Alloy Steel production concepts.
In HSLA steels, strength is derived from various mechanisms including solid solution strengthening, grain size refinement, and precipitation hardening. Precipitation effects can be substantial in hot rolled HSLA steels (HR HSLA)—facilitated by thermo-mechanical processing in the hot strip mill. Thus, HR HSLA steels are commercially available with minimum yield strength designations up to 700 MPa. Precipitation strengthening effects are generally less prominent for cold rolled steels, where solid solution strengthening and grain refinement dominate. This typically meant that hot rolled steels were available at greater strength levels than cold rolled steels. In the majority of the cold rolled high strength low alloy (CR HSLA) steel standards mentioned above, the strongest minimum yield strength designations are limited to 460 or 490/500 MPa. In 2024 the VDA 239-100 standard was expanded to include CR500LA and CR550LA.
Achieving Yield Strengths of 550 MPa and Beyond
Techniques to reach ≈ 500 MPa minimum yield strength in CR HSLA steels are well-understood and achievable with equipment and processing approaches that are globally available. These cold rolled steels are fully annealed above the recrystallization temperature to restore ductility lost during the cold rolling process.
For minimum yield strength levels above 500 MPa, automakers have typically relied upon advanced high strength steels (AHSS). At a given tensile strength level, AHSS typically have better global formability than HSLA steels (i.e. total elongation, n-value), while HSLA steels often have better local formability characterized by bendability and edge ductility (e.g. hole expansion ratio) [1].
There have been renewed interests in developing CR HSLA steels with yield strength exceeding 550 MPa—with a favorable balance of global and local formability as well as excellent weldability. For the purposes of this section, high strength low alloy steels with yield strength of at least 550 MPa will be collectively described as “Advanced HSLA” (AHSLA) steels, while in other contexts, the term “Super HSLA” has been used interchangeably [1]. Property requirements for AHSLA steels or for so-called ‘Super HSLA’ steels are not globally standardized, as the landscape is evolving. Table 1 shows example tensile property requirements for so-called ‘Super HSLA’ steels, proposed in 2025 [2].
Table 1: Proposed “Super HSLA” Tensile Property Requirements.
Based on Citation [2]
Proposed Grade
Yield Strength
Rp0.2 or ReL
[MPa]
Tensile Strength
Rm
[MPa]
Elongation
A50, Type I Bar
[%]
Nearest Equivalent
SAE J2340,
Rev March 2017
CR600LA
600 to 730
645 to 830
≥ 10
—
CR700LA
700 to 840
730 to 945
≥ 9
700 R
CR800LA
800 to 955
820 to 1055
≥ 8
830 R
Advanced HSLA Steels | Annealing Strategies
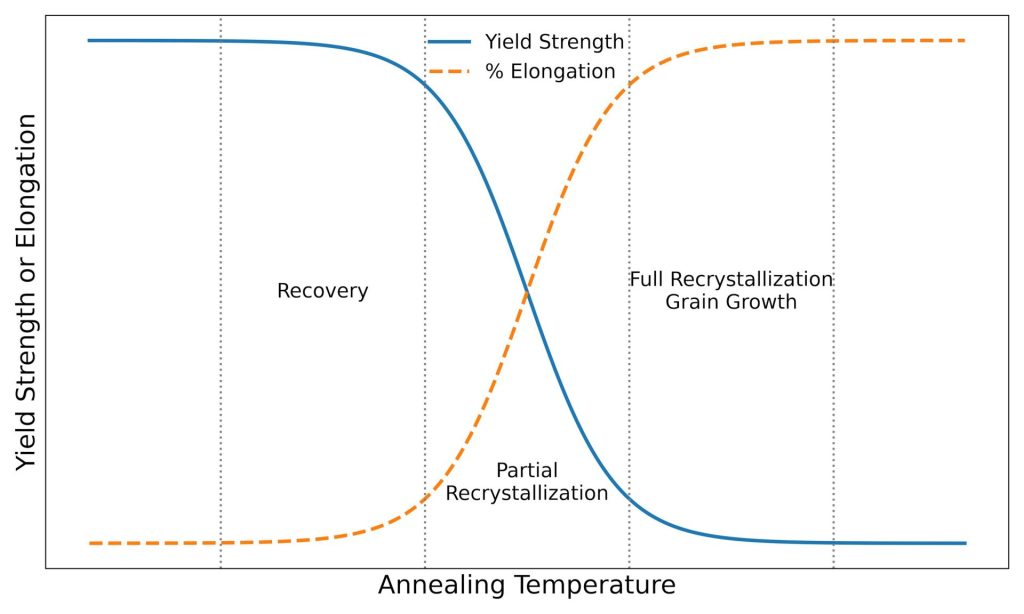
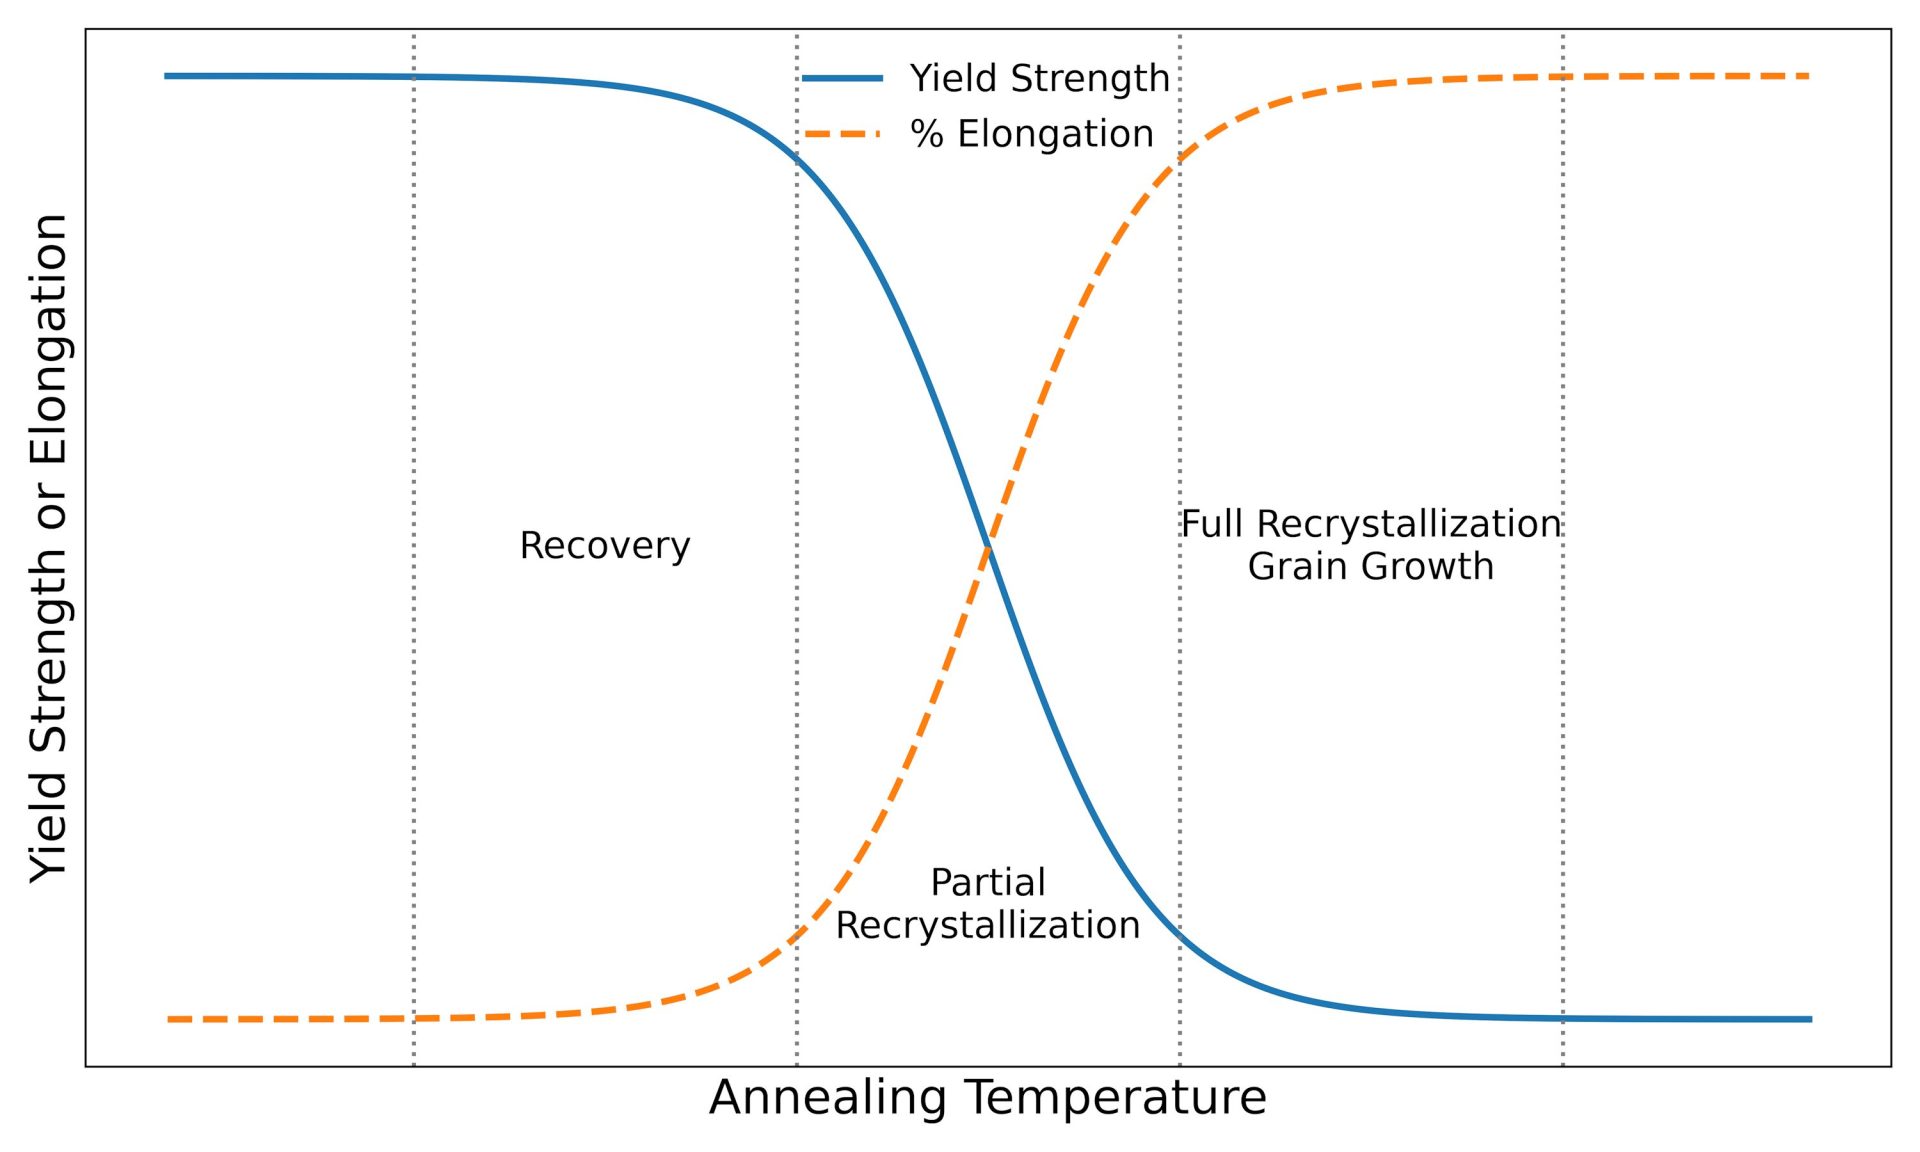
Part of the strategy deployed by steelmakers to extend the strength range of cold rolled, fine grained HSLA steels is to employ lower-temperature annealing practices known as recovery annealing and partial recrystallization annealing. In such processes, a portion of the cold rolled microstructure is preserved, thereby increasing strength relative to fully recrystallized steels.
The relative strength increase above that of a fully annealed cold rolled steel is inversely related to the annealing temperature. For example, in a low temperature process known as recovery annealing, the microstructural dislocation density is reduced, but the grain size, grain shape and grain distribution are effectively unchanged from the cold rolled condition. This process results in the highest strength CR HSLA products, at the expense of elongation. For a given recovery annealed grade, the yield strength and tensile strength are similar (high yield-to-tensile strength ratio). Recovery annealed grades are designated as ‘R-type’ grades in SAE Standard J2340, for example: 490 R, 550 R, 700 R and 830 R. They are also found in some grade specification documents released by Automotive OEMs.
At a somewhat higher temperature, yet still below the temperature for a full anneal, sufficient energy is imparted to convert a portion of the deformed grains to recrystallized grains. This partial recrystallization results in strength between that of a fully annealed product and that of a recovery annealed steel. The mixed microstructure contains both elongated and equiaxed grains and leads to a larger gap between yield and tensile strength than that observed in recovered steels–but not as large of a gap as found in fully recrystallized CR HSLA steels. Schematically, these concepts are shown in Figure 1.
Figure 1. Schematic showing yield strength and elongation as a function of annealing temperature for cold rolled HSLA steels (After [3]).
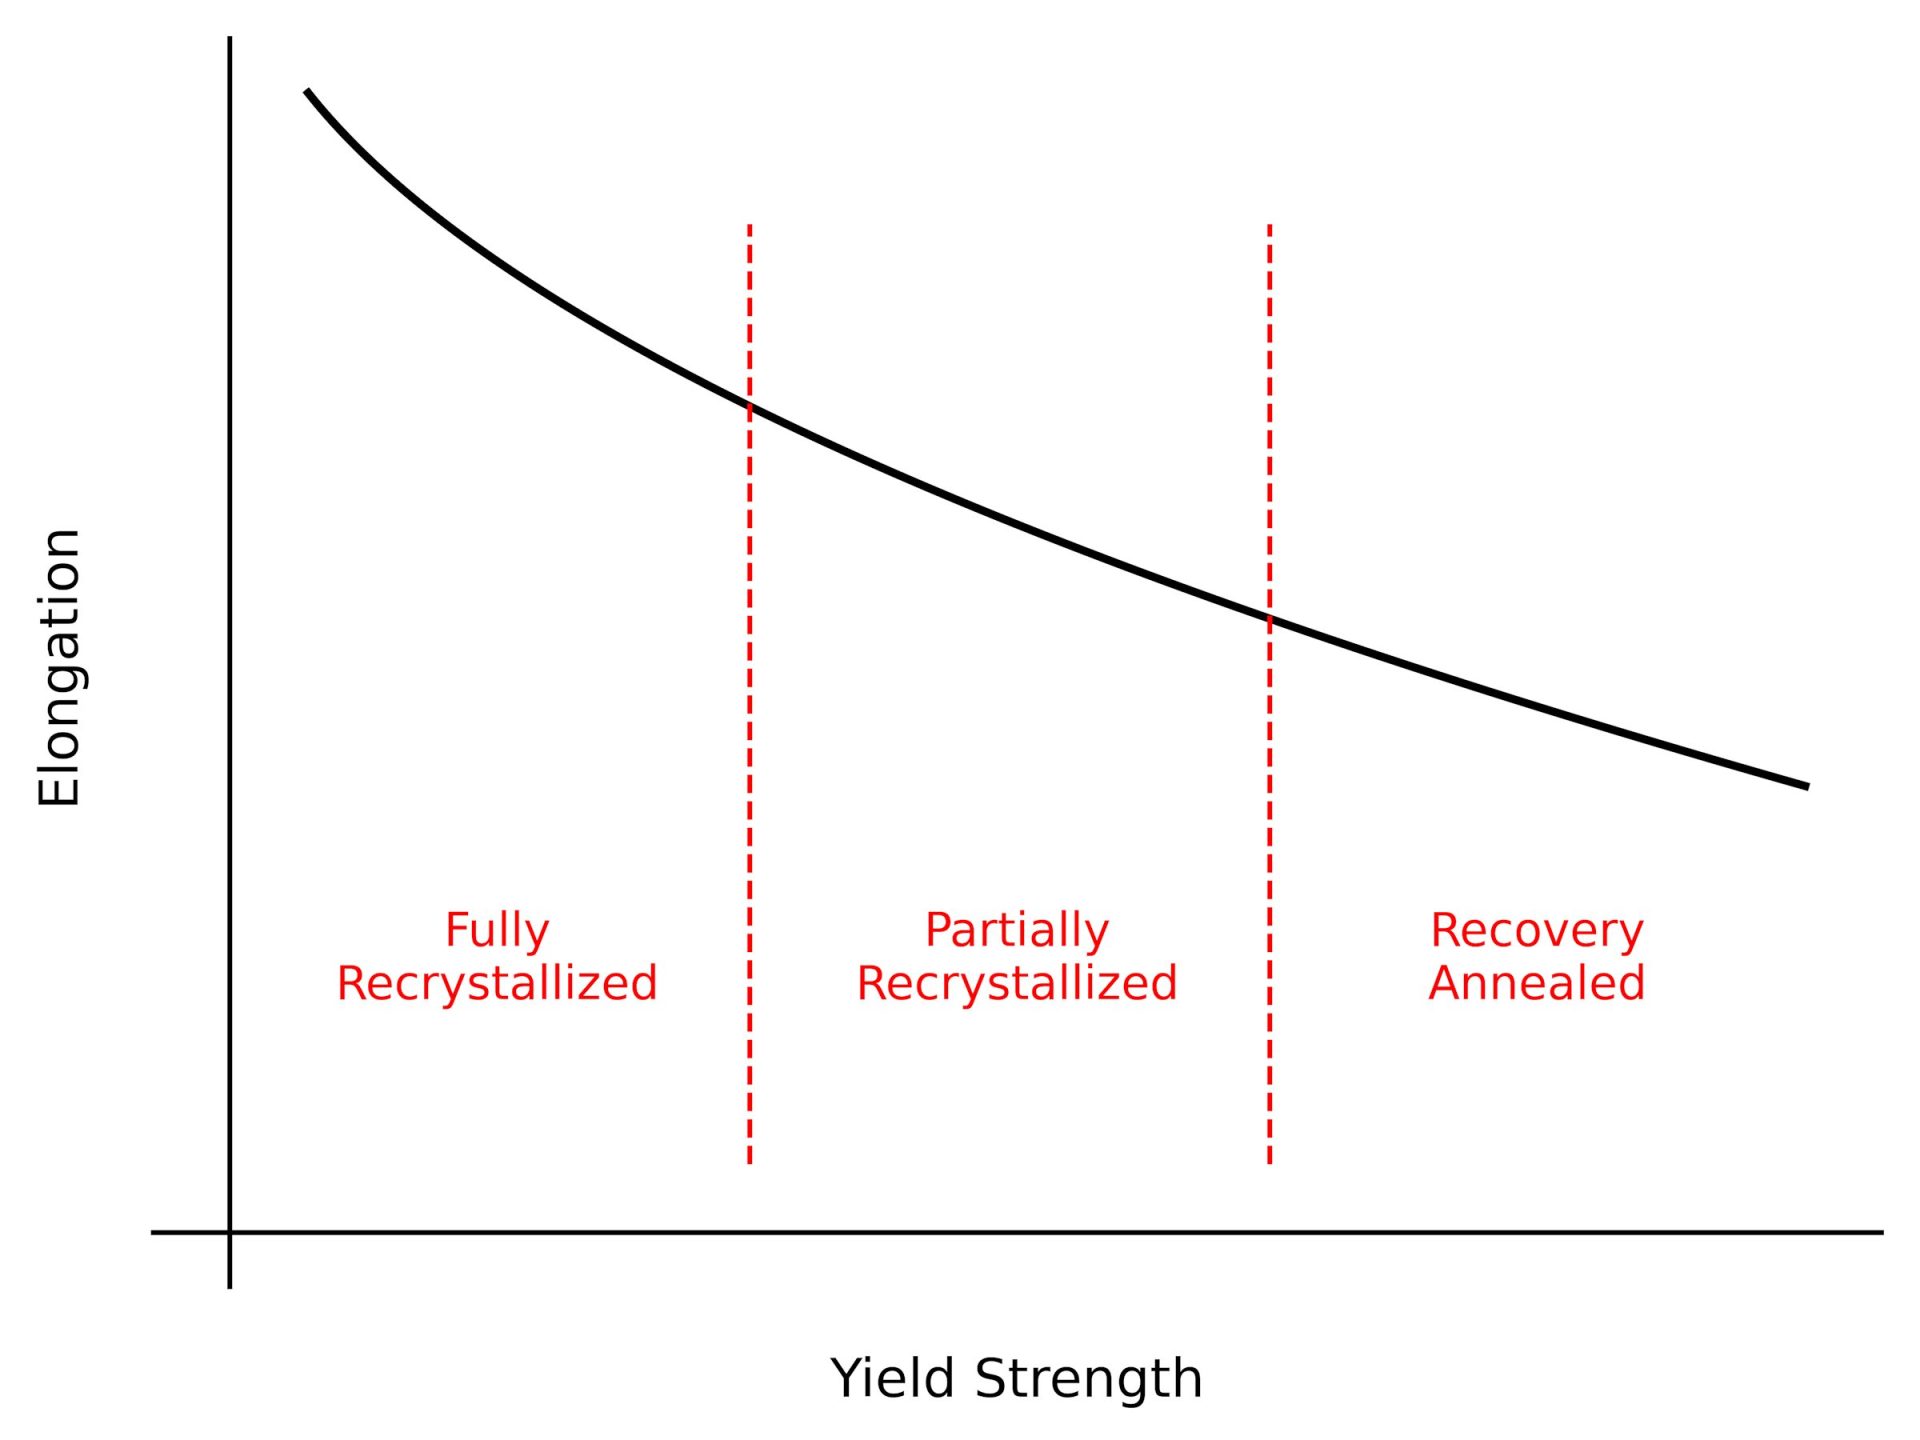
Another way of visualizing this relationship is to compare elongation and yield strength directly (Figure 2). Recovery annealing can produce the highest strength HSLA grades, but elongation will be lower than that associated with fully recrystallized HSLA products.
Figure 2: Schematic illustration of the influence of annealing strategy on elongation and yield strength of cold rolled HSLA steels (after [4]).
Advanced HSLA Steels | Process Parameters
While annealing temperature control is one lever available to steelmakers, steel composition (chemistry), percent cold reduction and annealing time also contribute considerably to the properties of the annealed product. In one approach niobium is added, either alone or in combination with molybdenum, to meet the targeted properties as shown in Table 1 for CR600LA and CR700LA [2][5]. Parameters associated with hot strip mill processing, cold rolling, and annealing are covered in [1], where various process paths for batch annealing, continuous annealing, and continuous hot-dip processing are discussed.
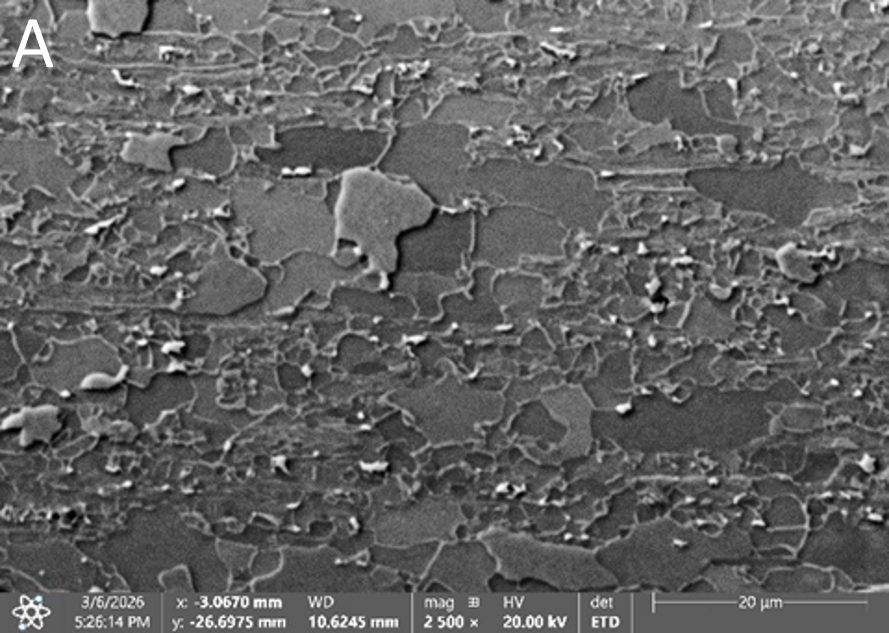
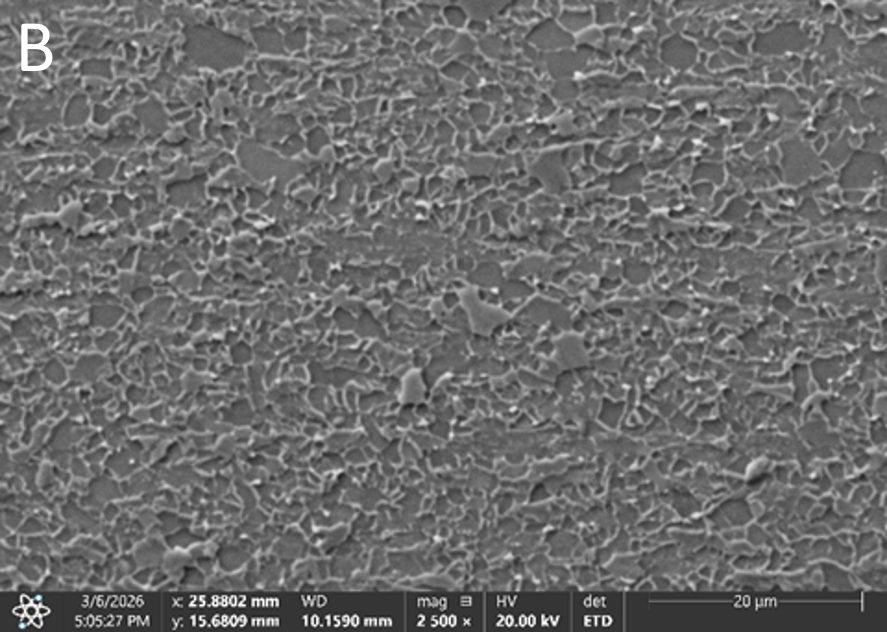
In another case it was demonstrated that CR550LA can be produced on an industrial hot-dip galvanizing line through multiple production strategies [11]. As an example, the relatively coarse, mixed microstructure shown in Figure 3A is the product of a partial recrystallization anneal, while that shown in Figure 3B is notably finer and more uniform. In the latter case, a higher annealing temperature and shorter annealing time (faster line speed) was prescribed to achieve a fine, uniform microstructure described as “rapidly transformed and cooled”. Both approaches resulted in properties consistent with CR550LA.
Figure 3A: Example microstructures of cold rolled HSLA steel (CR550LA) produced on an industrial hot-dip galvanizing line. (A) CR550LA produced via a partial recrystallization annealing cycle [11].
Figure 3B: Example microstructures of cold rolled HSLA steel (CR550LA) produced on an industrial hot-dip galvanizing line. (B) CR550LA produced with a higher-temperature, shorter-time annealing cycle (faster line speed) [11].
Global and Local Formability
Where global formability is the term given to necking-limited ductility parameters measured in a tensile test (elongation, n-value), local formability is the term given to fracture-limited formability parameters such as the hole expansion ratio (HER), the critical bending angle, and the minimum bending radius. Strength and local formability parameters of various AHSLA steels are listed in Citation [6] and reproduced in Table 2. The HER of these steels is at least as high as, and in some cases far superior to that of dual phase and complex phase steels of similar yield strength reported elsewhere [7].
Table 2: Strength and Local Formability Properties of Industrial Produced Steels.
Reproduced from CItation [6]
Property
Orientation
Continuous Annealing Line
Hot Dip Galvanizing
Batch Annealing
Nb
NbMo
Nb
NbMo
Nb
NbMo
Sheet thickness (mm)
1.3
1.3
1.3
1.3
2.5
2.5
Yield Strength
Longitudinal
650
690
600
690
700
800
Transverse
710
750
660
750
770
860
Hole Expansion Ratio (%)
86
81
87
68
74
69
Bending Angle (degree)
Longitudinal
117
106
111
106
114
95
Transverse
126
125
130
123
112
97
Bending Radius (Ri/t)
0.38
0.38
0.38
0.38
0.6
0.6
Additional strength, elongation and HER data for commercially-available AHSLA steels are shown in Table 3, which is based on [8].
Table 3: Strength and Local Formability Properties of Industrial Produced Steels.
Based on Citation [8]
Nominal Grade
Yield Strength
Rp (min)
[MPa]
Tensile Strength
Rm
[MPa]
Elongation
A80
[%]
Hole
Expansion
Ratio [%]
CR500LA
500
540 to 690
13
≈ 95 to 100
CR550LA
550
590 to 740
12
CR600LA
600
630 to 780
11
≈ 50 to 55
CR700LA
700
730 to 880
10
CR800LA
800
830 to 980
8
≈ 35 to 40
CR900LA
900
920 to 1070
7
CR1000LA
1000
1020 to 1170
5
≈ 25 to 30
Comparing HSLA and DP Steels of Similar Tensile Strength
Citation [9] presents a head-to-head formability analysis of CR550LA and CR590DP at similar tensile strength (both 1.5 mm thickness). As expected, the dual phase (DP) steel exhibits higher global formability (elongation, n-value), while the HSLA steel has a higher yield strength. Both have high intrinsic local formability (true fracture strain ≥1) with correspondingly good hole expansion ratios (~60%). This suggests that CR550LA may be a suitable alternative to CR590DP in applications where the added global formability of the DP steel is not required.
Table 4: Strength and Local Formability Properties of Industrial Produced Steels.
Based on Citation [9]
Grade
Yield
Strength
[MPa]
Tensile
Strength
[MPa]
Uniform
Elongation
[%]
Total
Elongation
[%]
n-value
r-bar
True
Fracture
Strain
Hole
Expansion
Ratio [%]
CR550LA
[HSLA]
609
657
10.5
18.4
0.100
0.86
≈ 1.21
≈ 58
CR590DP
[Dual Phase]
390
667
15.7
24.9
0.162
0.89
≈ 1.02
≈ 60
Visualizing an Alternative Global Formability Diagram
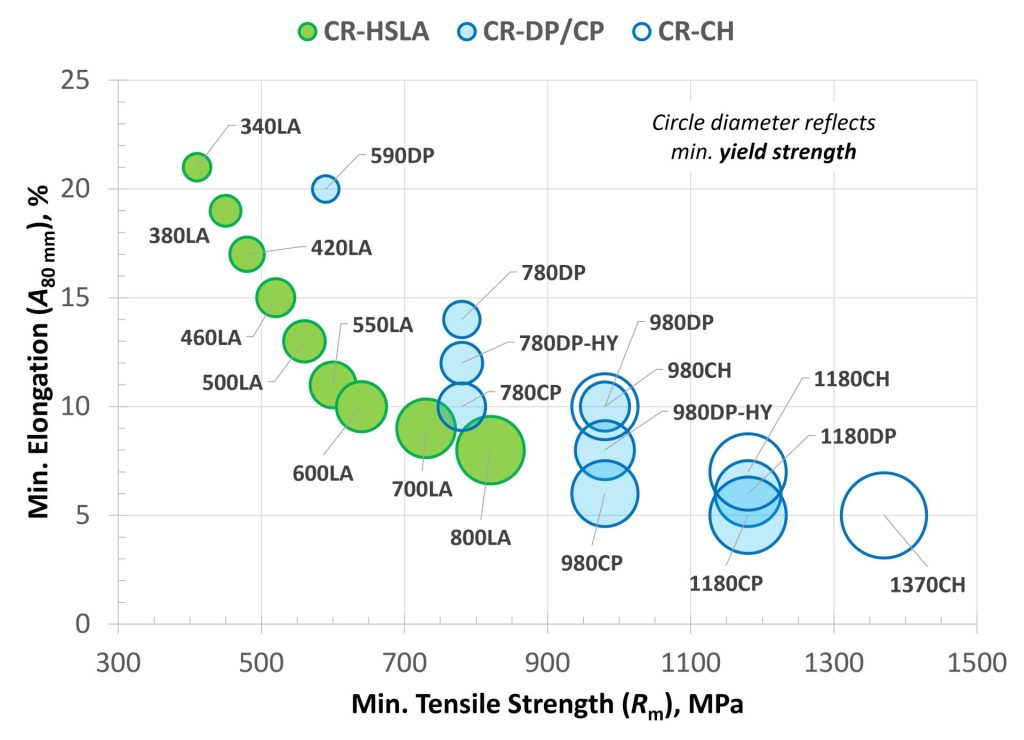
The traditional Global Formability Diagram illustrates the relationship between total elongation and tensile strength. Figure 4 is one such comparison, where the circle diameter reflects the minimum yield strength of each grade. This graph shows the basic rationale for AHSS (vs HSLA steels), where AHSS (blue) have better elongation at a given tensile strength than HSLA steels (green).
Figure 4: Traditional Global Formability Diagram based on the VDA 239-100 standard (minimum requirements), with the circle diameter proportional to the minimum yield strength of each grade. Also included are proposed “Super HSLA” grades [2].
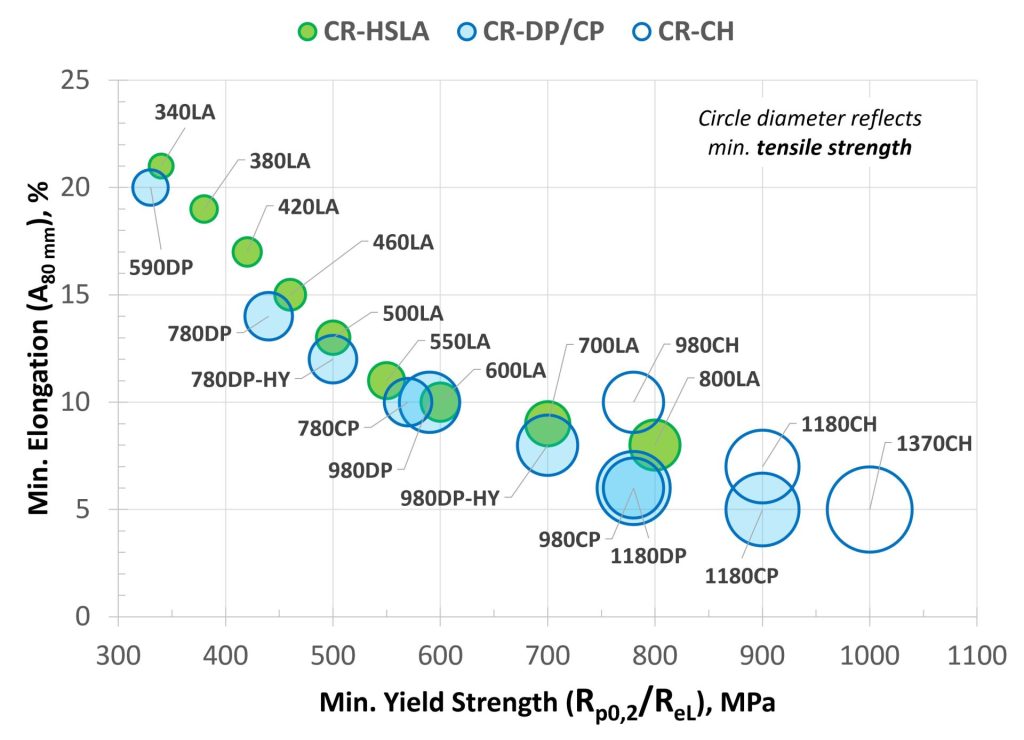
Alternatively, Figure 5 compares minimum elongation and minimum yield strength with the circle diameters proportional to the minimum tensile strength of each grade. When viewed this way, and for applications where as-delivered yield strength is critical, CR HSLA steels offer a competitive strength-elongation balance when compared to many CR AHSS grades (DP/CP types: filled blue circles). Also, at a given yield strength level, HSLA grades are expected to provide better local formability as characterized by bendability and hole expansion testing (HER).
Figure 5: Alternative Global Formability Diagram comparing minimum elongation and minimum yield strength. Here, the circle diameter reflects the minimum tensile strength for each grade. Note that the same data are represented in Figure 4 in the more traditional way (elongation vs tensile strength).
Visualizing the Balance Between Global and Local Formability
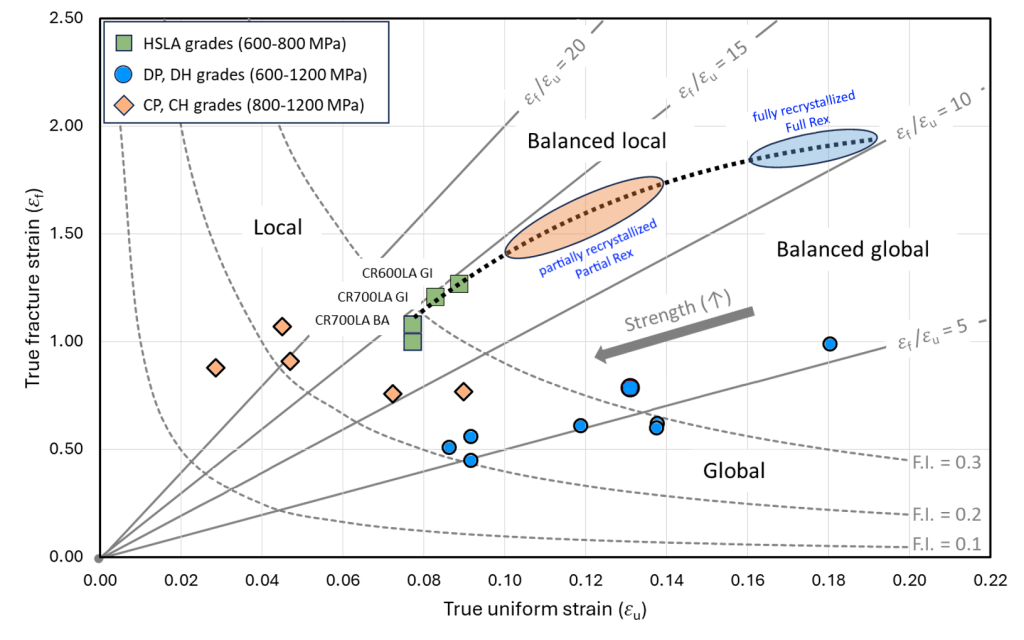
As described in Figure 4 in Defining Steels, the Local/Global formability map combines measures of local formability (true fracture strain) and global formability (uniform elongation), thus providing formability insights for various steel grades at a glance. This intrinsic formability mapping concept was extended in Citation [10] to include HSLA, DP, DH, CP, and CH grades, as shown in Figure 6.
The true fracture strain values of AHSLA (Super HSLA) steels (green squares) are generally higher than those of complex phase steels (CP/CH-type, orange diamonds) and dual phase steels (DP/DH type, blue circles).
Figure 6: Local/Global formability map illustrating the performance of Super HSLA steel relative to dual phase and complex phase steels of similar strength. Refer to [10] for details.
Expanding Supply Base
Earlier HSLA steels produced by integrated steelmakers relied on relatively high carbon content (sometimes 0.1% or greater) to help reach higher strength levels. Producers using thin-slab casting, typically found in electric arc furnace (EAF)-based mini-mills, often adopt a different metallurgical approach to reduce the risk of casting defects during continuous casting. This strategy typically includes maintaining carbon below approximately 0.08% to minimize peritectic solidification effects while carefully controlling microalloy additions to avoid excessive hot ductility loss as the strand undergoes bending and subsequent straightening in the curved section of the caster.
These compositional constraints, together with the need to maintain good castability, can make it increasingly challenging to achieve higher yield strengths in cold rolled steels using a thin-slab caster, particularly as yield strength requirements approach about 500 MPa. The subject AHSLA grades can be made with a relatively low overall alloy content, including carbon, thereby avoiding peritectic casting issues. For this reason, these grades are more suited to both thin slab and thick slab casting.
Automotive Applications
Cold rolled AHSLA (Super HSLA) steels, like other HSLA steels, feature a combination of strength, ductility, and weldability that is suitable for many automotive applications. Key characteristics include low carbon content and low carbon-equivalent together with a refined microstructure achieved through microalloying and thermo-mechanical processing.
Furthermore, the characteristically high as-produced yield-to-tensile strength ratio—often greater than 0.9 (90%)—ensures high yield strength throughout the formed part. This includes regions that experience little or no deformation and associated work hardening during forming. As such, these grades are particularly suitable for roll-formed components – for example roof bows or side intrusion protection beams. Other components that could benefit include those not subjected to the body-in-white (BIW) paint-baking process and therefore do not benefit from bake hardening.
Such applications include various automotive seating components (seat tracks, structural members), bumper beams and EV battery protection systems. The functional equivalence of AHSLA steels as viable AHSS alternatives in BIW crash energy management applications has not yet been clearly established.
Summary
Advanced High Strength Low Alloy (AHSLA) steels — also called “Super HSLA” — extend cold-rolled HSLA yield strength beyond the traditional ceiling of approximately 500 MPa by using recovery annealing or partial recrystallization annealing instead of a full anneal. These lower-temperature processes preserve part of the cold-rolled microstructure, trading some elongation for higher strength while keeping a high yield-to-tensile strength ratio (often >90%).
Compared to other AHSS at similar tensile strength, AHSLA grades show lower global formability (elongation, n-value) but comparable or better local formability (hole expansion ratio, bendability) plus better weldability due to lower carbon content and lower carbon-equivalent. Low carbon content, typically less than ≈0.08%, also makes these grades well suited to both thick-slab and thin-slab casting, broadening the potential supplier base beyond integrated mills.
For automotive engineers, the practical appeal of AHSLA steels is that parts retain strength uniformly even in low-deformation zones, since final part strength comes from processing and chemistry rather than from work hardening or bake hardening. Limited strain hardening response also supports better dimensional control across a formed part, making AHSLA grades attractive for components where high strength is needed for structural and crash benefits. Such applications include those which are roll-formed or do not benefit from the strengthening that comes from paint-baking, e.g. seat tracks and structural members, bumper beams, and EV battery protection structures.
[2] B.M. Hance and H. Mohrbacher, “Optimization of global and local formability properties through Nb microalloying,” Presented at 3rd Automotive Steel International Conference AISTech, 9–12 March 2025, Orlando, Fla., USA, 47-53.
[5] H. Mohrbacher, M. Ploberger, G. Ischia, S. Gialanella, and T. Hebesberger, “Annealing response and yielding behavior of cold rolled advanced HSLA steels,” Materials Science and Engineering: A, Volume 903, 2024,146666; https://doi.org/10.1016/j.msea.2024.146666.
[7] A. Karelova, C. Krempaszky, E. Werner, P. Tsipouridis, T. Hebesberger and A. Pichler, “Hole Expansion of Dual-phase and Complex-phase AHS Steels – Effect of Edge Conditions,” Steel Research International, Volume 80, Issue 1, 2009, pp.71–77; https://doi.org/10.2374/SRI08SP110.
[9] H.-C. Shih, L. Brown, V. Pednekar, M. Shi, and S. Tedesco, “Comparison of Formability Performance Between CR550LA and CR590DP,” WCX SAE World Congress Experience, Detroit, Michigan, United States, April 14, 2026; https://doi.org/10.4271/2026-01-0178.
[11] C.M. Enloe, K. Bhadhon, F. Perez Meza, R. Osei, S. Samantha, J.G. Speer, B.M. Hance and V. Giorgetti, “Development of Cold-Rolled, Hot-Dip Galvanized HSLA Steel with 550 MPa Minimum Yield Strength,” Presented at the 9th International Conference on Recrystallization and Grain Growth (ReX&GG), Hamilton ON, Canada, May 25-26, 2026, used with permission.
Thanks are given to Brandon Hance, Ph.D., for his contributions to the Advanced High Strength Low Alloy steel section. Dr. Hance has dedicated more than 30 years to the automotive industry focused on the mechanical and physical metallurgy of high-strength steels. In his most recent role at CBMM North America, he supported customers from material grade development through industrial implementation. Before that he served as Vice President & Head of the Applications Engineering Group at Hyundai Steel Company in South Korea, as well as in prior R&D roles at United States Steel Corporation, AK Steel Corporation, The Timken Company and Novelis. Brandon has a PhD degree in Materials Science from the University of Pittsburgh, an MS degree from the Colorado School of Mines, and a BS degree from the Illinois institute of Technology. He currently volunteers as Secretary of the North American Deep Drawing Research Group (NADDRG) and is the USA Representative to the International Deep Drawing Research Group (IDDRG).
Mild steels are low carbon steels with no alloying elements added for substantial strengthening, and for that reason are characterized by relatively lower yield strength. Typically, mild steels have less than 0.10% carbon.
These steels have a microstructure that is primarily ferrite. The amount of pearlite in the microstructure is a function of the amount of carbon in the steel, with lower carbon resulting in a lower fraction of pearlite. More information about microstructural components is available here.
Ultra-low carbon steels are a type of mild steel. These grades are typically the lowest yield strength and highest ductility available. Generally, these steels have less than 0.005% carbon, or less than 50 ppm C. More information is contained on the page for Ultra-Low Carbon steels.
Different names may describe mild steels, but these differences came from steel mill production techniques that are no longer in use. Since all sheet steels in use today are continuously cast, there are no significant differences between these terms:
Drawing Quality (DQ)
Drawing Steel (DS)
Aluminum Killed Drawing Quality (AKDQ)
Drawing Quality Aluminum Killed (DQAK)
Drawing Quality Special Killed (DQSK)
Mild steels are described in OEM, regional or global specifications with different syntax. While certain grade definitions between these specifications may be similar, the user is cautioned against using conversion charts without first confirming aspects which might be different, such as minimum, maximum, or typical values of chemical or mechanical properties. For example, ASTM specifications which cover lower strength steels list only typical values for tensile properties, but these are non-mandatory and the user may receive product outside the ranges shown. Additionally, JIS specifications which cover lower strength steels do not have minimum yield strength requirements, and the minimum elongation varies by thickness.
Some of the specifications describing uncoated cold rolled mild steel are included below, with the grades typically listed in order of increasing ductility. Different specifications may exist which describe hot or cold rolled, uncoated or coated, or steels of different strengths. Many automakers have proprietary specifications which encompass their requirements.
ASTM A1008M, with the terms CS, DS, DDS, and EDDSA-25
EN10130, with the terms DC01, DC03, DC04, DC05, and DC06D-3
JIS G3141, with the terms SPCC, SPCD, SPCE, SPCF, and SPCGJ-2
JFS A2001, with the terms JSC270C, JSC270D, JSC270E, JSC270F, and JSC260GJ-23
VDA239-100, with the terms CR1, CR2, CR3, CR4, and CR5V-3
Bake Hardenable (BH) steels grades are conventional High Strength Steels that exhibit a Bake Hardening Effect. BH steels exhibit an increase in yield strength after room-temperature stamping followed by processing through a thermal cycle comparable to the time-temperature profile used in paint curing (or baking) – approximately 170 °C for 20 minutes. Bake hardenability is characterized by determining the Bake Hardening Index.
Bake Hardenable steel grades have yield strength at shipment from the steel mills of 180 MPa to 300 MPa (approximately 25 ksi to 45 ksi). The grades at the lower strength levels are capable of being produced with a Class A surface finish and are used in applications where dent resistance is desired in thin sheet steel. Applications for the higher strength BH steels include structural parts where Class A surface is not required. The higher strength after forming and baking is the reason automakers might use these in body structure applications, potentially contributing to vehicle lightweighting efforts.
These grades work harden approximately 30 MPa when 2% strain is introduced, either from stamping or during a tensile test, which is similar to dent resistant IF-HS. In contrast to IF-HS, the paint-bake cycle after forming results in an additional yield strength increase. The minimum strength increase from baking is specified by some automakers as 20 MPa to 35 MPa, measured after applying a defined level of strain.
Higher yield strength directly improves the dent performance. Even though BH grades and their non bake hardening counterpart IF-HS grades may have similar yield strength and thickness after forming, bake hardenable steels will show superior dent resistance due to the increase in yield strength from the paint baking operation.
Ferrite is the main microstructural phase of BH steels. The strengthening from the paint bake cycle is due to the controlled amount of carbon remaining in solid solution (on the order of 25 ppm) when the steel leaves the production mill. At the baking temperatures after the part is formed, the dissolved carbon migrates to pin any free dislocations created from stamping. This increases the yield strength of the formed part for increased dent resistance. Formability does not suffer, since the strength increase occurs after stamping.
Most Advanced High Strength Steel (AHSS) grades also exhibit a Bake Hardening Effect, achieving yield strength increases of 40 MPa to 120 MPa from an appropriate thermal cycle. AHSS grades are not categorized with traditional bake hardenable steels, since their primary characteristics and applications are typically, but not exclusively, different. One exception are some Dual Phase (DP) steels available with a Class A surface, which are used as skin panels to combine excellent dent resistance with lightweighting benefits.
Some of the specifications describing uncoated Bake Hardenable (BH) steel are included below, with the grades typically listed in order of increasing minimum yield strength and ductility. Different specifications may exist which describe uncoated or coated, or steels of different strengths.
ASTM A1008M, with the terms BHS 26 [180], BHS 31 [210], BHS 35 [240], BHS 41 [280], BHS 44 [300]A-25
EN10268, with the terms HC180B, HC220B, HC260B, and HC300LAD-3
VDA239-100, with the terms CR180BH, CR210BH, CR240BH, and CR270BHV-3
Bake Hardening Effect
Bake Hardenable Steel Grades and most AHSS grades exhibit a Bake Hardening Effect, meaning that there is an increase in yield strength after room-temperature stamping followed by processing through a thermal cycle comparable to the time-temperature profile used in paint curing (or baking) – approximately 170 °C for 20 minutes.
The degree to which a sample is bake hardenable is characterized by the Bake Hardening Index.
In Bake Hardenable Steel Grades, solid solution hardening elements like phosphorus, manganese, and silicon are used to achieve the desired initial strength. For AHSS, the initial strength is determined by the balance and volume fraction of microstructural components like ferrite, bainite, retained austenite, and martensite. In both cases, a specifically engineered amount of dissolved carbon in the ferritic matrix causes an additional increase in the yield strength through controlled carbon aging during the paint-bake thermal cycle. The bake hardening process in AHSS grades is more complex, and results in substantially higher values of the Bake Hardening Index.
Figure 1 shows the work hardening and bake hardening increases for samples of three High-Strength steel grades having the same as-received yield strength prior to 2% pre-straining and baking. The HSLA steel shows little or no bake hardening, while AHSS such as DP and Transformation Induced Plasticity (TRIP) steels show a large positive bake hardening index. The DP steel also has significantly higher work hardening than HSLA or TRIP steel because of higher strain hardening at low strains. No aging behavior of AHSS has been observed due to storage of as-received coils or blanks over a significant length of time at normal room temperatures. Hence, significant mechanical property changes of shipped AHSS products during normal storage conditions are unlikely.
The higher bake hardening index (BHI) of AHSS grades DP 600 and TRIP 700 is also shown in Figure 2. While BHI is determined at a prestrain of 2%, this graph indicates that even higher levels of bake hardenability can be achieved with increasing strain. In a stamping where most areas have more than 2% strain, combining this higher bake hardenability with the increased work hardening that occurs with increasing strain results in a formed panel having a strength markedly higher than the incoming flat steel. This is beneficial for crash energy management.
Figure 1: Comparison of work hardening (WH) and bake hardening (BH) for TRIP, DP, and HSLA steels given a 2% prestrain. S-1, K-3
Figure 2: Bake hardening responses of several HSS and AHSS products with varying pre-strain, reproduced from Figure 3 in Citation B-6. The bracketed numbers after each grade are references within the cited paper.
Bake Hardenability of Exposed Quality Dual Phase Steels
Dent resistance is a function of the yield strength in the formed panel after it completes the paint baking cycle. Based on this premise, grades with higher bake hardenability, such as AHSS, should have substantially higher dent resistance. Application of AHSS grades to capitalize on improved dent resistance also requires their production at the desired thickness and width along with surface characteristics appropriate for Class A exposed quality panels. Some DP steels meet these tight requirements specified by the automotive industry.
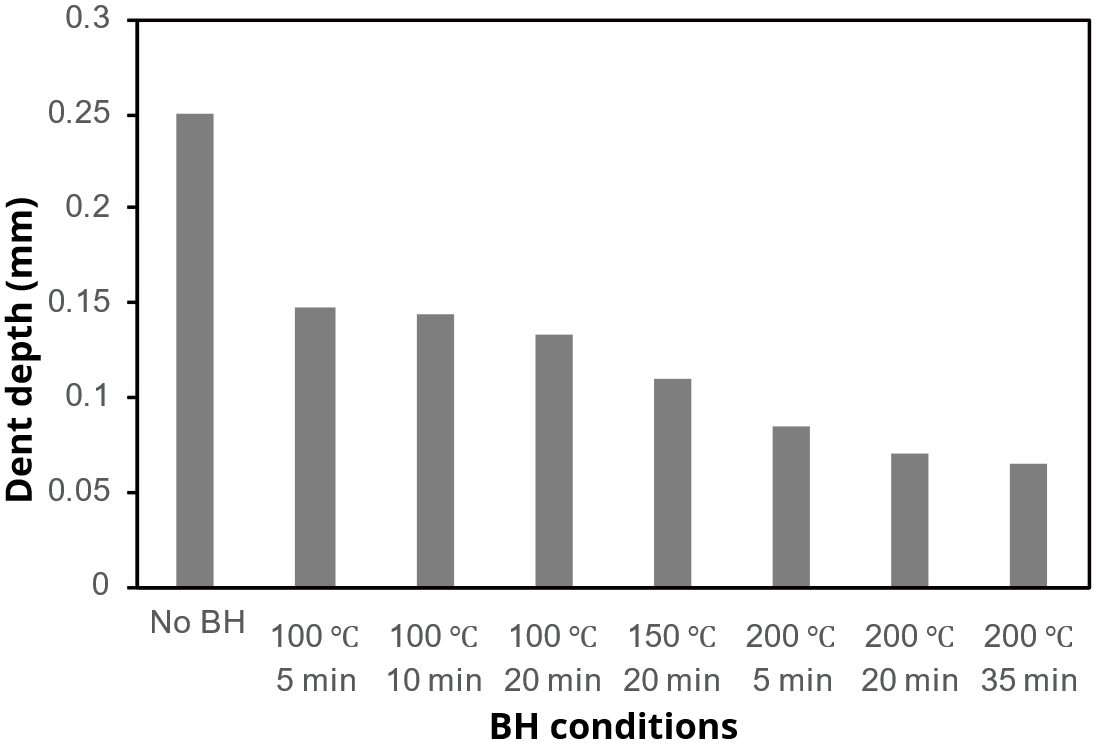
A recent studyK-49 highlights this improved dent resistance. This work presents the experimental results and associated numerical investigation of the dent testing of DP270Y490T, a DP steel grade with 490 MPa minimum tensile strength. Tests performed to the SAE J2575 procedureS-7 measure the resultant dent depth after testing, so therefore smaller depths indicate improved performance. Compared with samples not processed through a bake hardening cycle, dent depth reductions occur with hotter and longer cycles, as shown in Figure 3. Increasing temperature plays a more significant role in dent depth reduction than increasing time. This work also reinforces that bake hardenability must be incorporated into simulation models in order to improve the accuracy of dent resistance predictions.
Figure 3: Dent resistance of DP270Y490T according to SAE J2575S-7 as a function of baking test conditions.K-49 Lower dent depth indicates better dent resistance.
Bake Hardenability of 980 MPa and 1400 MPa Multi-Phase Steels with Different Prestrains
Citation X-5 evaluated the bake hardenability as a function of pre-strain on two steels having a microstructure of ferrite and martensite. The two steels are distinguished by their tensile strength: Test steel 1# is a 980 MPa grade with a yield:tensile ratio of 80%, whereas test steel 2# is a 1400 MPa grade with a yield:tensile ratio of 85%. See Table 1 for details.
Steel
ID #
Thickness
(mm)
Yield Strength
(MPa)
Tensile Strength
(MPa)
Elongation
(%)
Elongation at Break
(%)
1#
1.5
832
1047
7
13.5
2#
1.4
1243
1455
4
7
Table 1: Mechanical Properties of Tested Steels. X-5
Conventional uniaxial tensile testing of a #5 JIS bar was used to apply prestrain and evaluate mechanical properties. After pre-straining, samples were tested by first bending coupons to 90°, followed by the conventional paint bake thermal cycle of 170 °C for 20 minutes except for the control samples which remained unbaked. In all cases, the bend line was parallel to the rolling direction.
In the absence of prestrain, no bake hardening was observed in the two steels, indicating that prestrain is a prerequisite for promoting bake hardening.
Increasing levels of prestrain did increase the bake hardening response, but only to a certain level, with the two steels having a different prestrain response. The lower strength Steel 1# reaches a maximum BH value of approximately 80 MPa at a prestrain of 2%, while the higher strength Steel 2# reaches a maximum BH value of approximately 160 MPa at a prestrain of 1%. See Figure 4.
Figure 4: Effect of prestrain on Bake Hardening of 980 MPa and 1400 MPa steels.X-5
The elongation to fracture response to increasing prestrain is found in Figure 5, which shows a continuous decrease in ductility.
Figure 5: Effect of prestrain on Elongation of 980 MPa and 1400 MPa steels.X-5
Using these grades in production applications requires the formed product to be capable of withstanding additional damage if involved in a crash. As such, some coupons bent to 90° were baked while others remained unbaked, and all were subsequently bent another 30°, producing a final bending angle of 60°.
Baking has an adverse effect on the secondary bending performance of the 1400 MPa grade, which required a bend radius of 3 mm to avoid bend cracks in the baked condition. Without baking, a 2 mm radius was successfully bent. In the 980 MPa grade, no cracking was found even with a 1 mm radius in either the unbaked and baked conditions.
Measuring The Bake Hardenability Index
Bake hardenability is characterized by determining the Bake Hardening Index, or BHI.
The Bake Hardening Index (BH2) is determined by taking a conventional tensile test sample and pulling it to 2% strain. This is known as a 2% pre-strain. The sample is then put into an oven for a thermal cycle designed to be typical of an automotive paint curing (paint baking) cycle: 170 °C for 20 minutes. The temperature and time may be different depending on the end-user specifications.
Some companies may specify BH0, which uses the same thermal cycle without the 2% pre-strain. BH5 or BH10 (5% or 10% pre-strain, respectively) may also be reported.
The experimental procedure and calculation of BH2 is standardized in EN 10325D-4 and JIS G 3135J-3, and is similarly described in several other specifications.
Figure 6 defines the measurement for work hardening (B minus A), unloading to C for baking, and reloading to yielding at D for measurement of bake hardening (D minus B). Note that the bake hardening index shown here is measured up to the lower yield point, which is consistent with the EN 10325 definition. JIS G 3135 prescribes the use of the upper yield point.
Figure 6: Measurement of work hardening index and bake hardening index. BHI is measured using the lower yield point in EN 10325D-4 and with the upper yield point in JIS G 3135J-3.